Environment
Near-zero emissions thanks to the 18-PCS system, 98 % reduction in waste volume, and 90 % reduction in weight.

Controlled neutralization, high-temperature thermal destruction, and total regulatory compliance.
At INCINERO KBH, managing hazardous chemical waste is governed by strict HSE excellence, advanced gas scrubbing technology, and full compliance with Algerian environmental laws.
INCINERO KBH's health, safety, and environment policy is built on a structured management system and a continuous improvement approach.
It aims to eliminate risks for our employees, partners, communities, and the environment, while ensuring responsible management of special and hazardous special waste.
We are building a culture in which every team member plays an active role in accident prevention, risk reduction, and minimising our environmental impact.
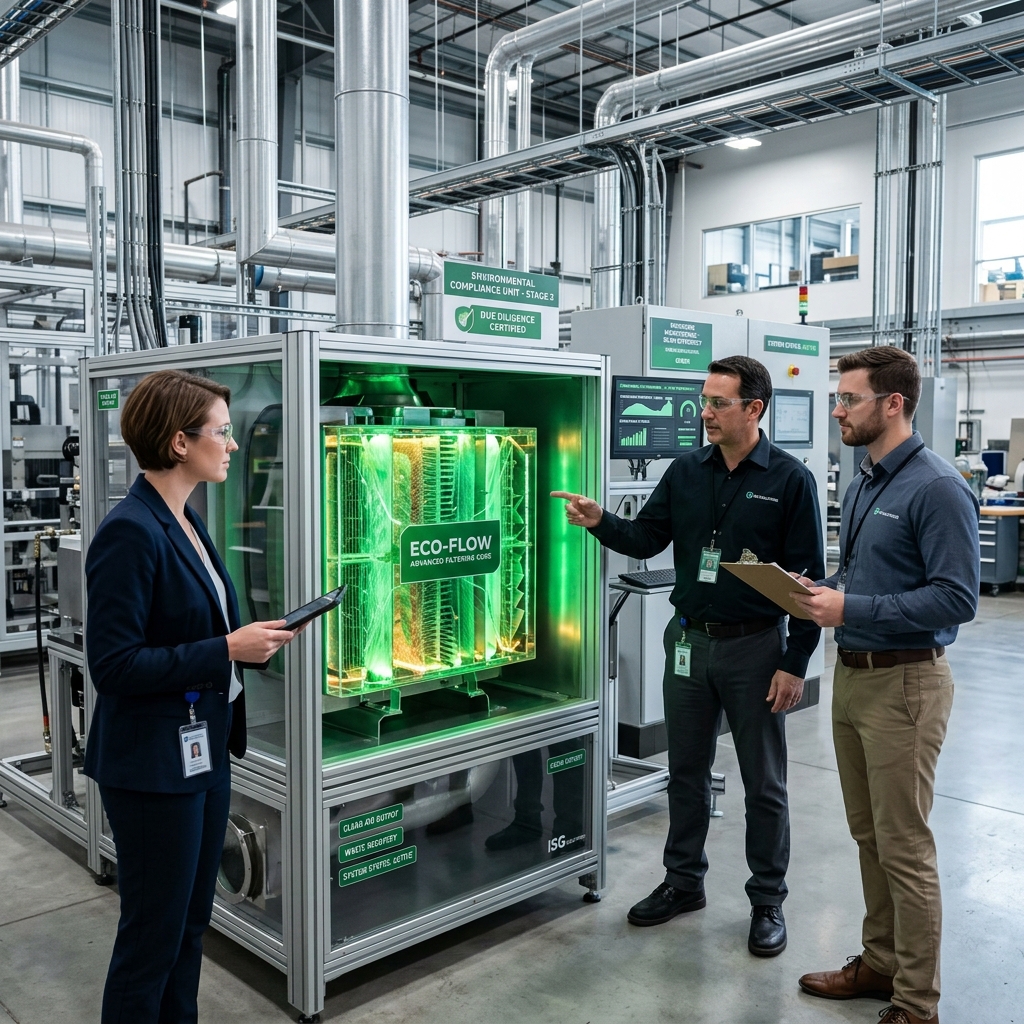
To protect the environment:
Efficient energy use and preservation of natural resources.
Continuous reduction of our emissions, effluents, and waste across all our sites.
Project life cycle analysis and selection of the best available technologies (including our 18-PCS system).
We encourage suppliers and subcontractors to adopt the same responsible standards.
Near-zero emissions thanks to the 18-PCS system, 98 % reduction in waste volume, and 90 % reduction in weight.
Full traceability, ongoing training, certified equipment, and strict procedures to protect our teams and local communities.
ISO 9001, CE marking, Ministry of Health approval, and compliance with Algerian and international standards.
Regular evaluation of our performance and implementation of corrective actions.
The neutralization and compliant disposal of chemical waste in Algeria (solvents, acids, alkalis, contaminated effluents) require absolute operational precision. INCINERO KBH enforces a 4-step safety protocol guaranteeing zero environmental risk on site and throughout ADR transport.
Prior SDS verification and laboratory compatibility testing (acid/base, oxidizer/reducer) before acceptance and batch loading.
UN-approved leakproof containers (HDPE drums, 1000L IBCs, stainless tankers), ADR-trained drivers, and full BSD tracking manifests.
Precise pH adjustment, heavy metal chemical precipitation, and decantation of industrial baths prior to thermal processing.
High-temperature destruction at 1200°C paired with our 18-PCS flue gas cleaning system that captures acid gases and heavy metals.
We handle all industrial chemical streams: halogenated and non-halogenated spent solvents, concentrated acidic and alkaline baths, expired laboratory reagents, chemical effluent treatment sludge, and agrochemical or pharmaceutical residues.
Transportation is strictly managed under international ADR regulations using UN-certified packaging, spill response kits, ADR-trained drivers, and mandatory BSD tracking manifests.
Our high-temperature A4000 thermal plant features an 18-PCS ceramic filtration and reagent injection system that neutralizes acid fumes (HCl, SO2, HF) and captures heavy metals to ensure near-zero atmospheric emissions.